


Views: 154 Author: Lucian Publish Time: 2026-08-26 Origin: Site


Residual solvent leaves a pattern
When the same blind hole is wet after every cycle, more drying time may only treat the symptom. Purchasing managers and process engineers can use where the liquid follows to decide whether the part, basket or machine needs attention.

Scope of this diagnosis: this page isolates loading and basket geometry. It does not diagnose vacuum-pump faults, rewrite the solvent recipe or make a general stainless-steel grade recommendation.
A longer cycle can evaporate solvent that should have drained earlier, but it also adds cycle time to every future batch. Opening the basket indiscriminately may weaken part retention and require another sample without changing an upward-facing blind hole. Before approving either action, preserve the failure evidence: photograph the wet part before unloading, record its basket position and mark the cavity or contact face where liquid remains.
The location must repeat before it can support a design decision. One wet part in one cycle may come from loading variation. The same liquid pocket after controlled position changes is much stronger evidence. That distinction matters during project acceptance because an unnecessary basket revision can delay release while the actual machine or process condition remains unresolved.
Decision rule: change the basket only when the wet location follows a repeatable part orientation or basket contact point while the machine cycle remains unchanged.
Wet parts per load and the repeated wet location
Extra drying minutes or repeat cycles
Rework hours and any delay to production release
Hydrocarbon or modified-alcohol solvent dissolves oil and grease after it reaches the metal surface. Ultrasound produces cavitation in the liquid, but it cannot clean the inside of a cavity that remains air-bound or is sealed against another part. The loaded orientation therefore has to let gas leave as solvent enters. A divider that holds two oily faces together can defeat that wetting step even when the basket is fully immersed.
After cleaning, gravity should remove the free liquid. Reduced pressure lowers the solvent's boiling temperature so the remaining film can evaporate during vacuum drying. A pool in an upward-facing bore contains far more liquid than a surface film, and a narrow outlet can restrict both drainage and vapor escape. Heat and vacuum may eventually dry it, but the machine must spend longer correcting a geometric problem.
A degreasing machine basket controls that geometry. The basket must retain the smallest component, separate contaminated faces, vent internal cavities and hold drain points below the liquid they release. Its frame must also remain seated on the machine supports under the actual load. Fine mesh, broad rails and close dividers are useful only where their retention or protection benefit is greater than the access and drainage they remove.
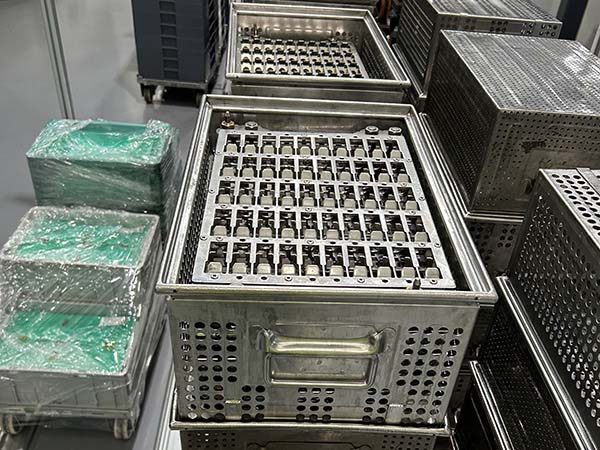
This loaded AUKE basket makes the first purchasing question visible: does each part have a defined position, or can a bore rotate upward during handling? Open basket walls help solvent move through the load, but they cannot correct an unstable part angle.
Use the same part count, orientation and machine cycle. If the wet location does not repeat, loading variation or an intermittent process condition is more likely than one fixed basket feature.
Move the wet part to another basket position without changing its orientation, then put another part in the original position. Liquid that follows the cavity points to part geometry or angle. Wetness that remains behind the same rail or retainer points to the basket position.
Return the part to the original basket position and rotate it without changing the cycle. If the wet point disappears or moves, the support angle is controlling drainage. If the whole load is wet, investigate solvent condition, temperature, vacuum level and cycle performance before altering the basket.
Confirm what remains on the surface before using its appearance as evidence. An oil film at a contact face supports an access problem; retained cleaning solvent in an otherwise clean cavity supports a drainage or drying problem. Recontamination after unloading is a third condition and should not trigger a basket redesign.
Send the three test results to AUKEOnce the cross-over comparison points to the basket, we place the wet location on the part drawing and overlay the support, retainer and mesh beneath it. This turns a general complaint into one design variable: outlet clearance, part angle, contact width, mesh opening or loaded support height.
The modification is kept local where possible. Raising one contact may uncover the outlet, but the new support must still retain the part and avoid a finished face. Replacing a solid ledge with spaced wire may improve solvent access, but the wire diameter and spacing must carry the load. Opening a true low point helps only when the smallest component cannot escape through it.
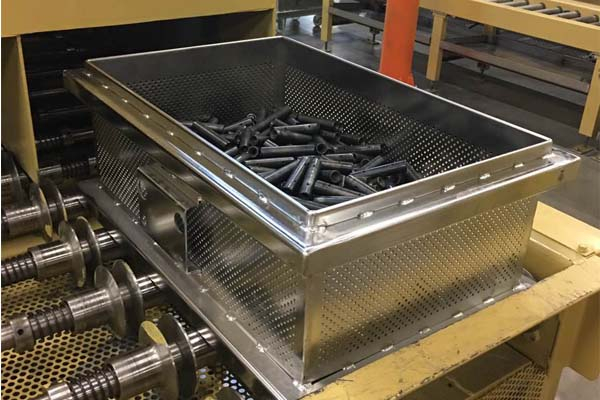
Open walls provide broad solvent access, but a part that can roll into a liquid-trapping angle may still need a dedicated support or divider.
Material and finish are considered at the same failed location. For this application, the stated maximum is 95°C, but temperature alone cannot select the stainless steel grade. Solvent composition, additives, metallic fines, exposure frequency and part material can change the compatibility requirement. Smooth, accessible joints also matter because a narrow weld crevice can retain contaminated liquid even when the surrounding mesh drains freely.
We run the revised sample with the original part count, orientation and machine cycle. It passes only when the original pocket is dry, every part remains retained and no new contact mark or wet location appears. The machine settings stay unchanged during this trial so the result can be attributed to the basket revision.
A successful sample is not enough if the next batch moves the corrected support back into the drain path. The controlled drawing therefore identifies the support height relative to the outlet, the approved part angle, the clear opening after bending and the machine contact points that establish the loaded basket position.
Those characteristics lead to practical production controls. A locating fixture can hold a representative part while support clearance is measured. The finished basket can be seated on its machine-contact points while base flatness and the critical angle are recorded. Drain openings are examined after forming and welding, when distortion is already present, rather than only on the flat cut piece.

This AUKE production image shows spacing measured on the finished support assembly. In a drainage correction, the recorded dimension must connect the part outlet to the support that holds its angle after forming and welding.
AUKE's published full-vacuum basket project used stainless steel baskets with modified alcohols and non-halogenated hydrocarbons. The documented design combined a load-bearing frame, welded wire construction, a lid and machine-compatible dimensions. It demonstrates relevant interface and fabrication experience without suggesting that every wet-part problem has the same cause.
AUKE supports custom dimensions, mesh, dividers, lids, handles and part supports, with trial quantities available before repeat orders. For this article's problem, the value of that flexibility is precise: only the feature linked to the residual-solvent pattern needs to change.
The most useful failure photographs are taken before the parts are removed. One close view should show the wet cavity or surface, while another should show the complete loaded basket and its position in the machine. The current basket drawing, part drawing, loaded weight and machine support dimensions connect the photograph to the physical arrangement.
Process information keeps the basket discussion honest. Share the solvent family, ultrasound use, maximum temperature, vacuum-drying sequence, part count and whether the wet location repeats from cycle to cycle. From those details, we can separate basket-controlled variables from symptoms that belong with the equipment team.
The useful output is a specific judgment: the likely source of the liquid pocket, the basket feature connected to it, the tradeoff created by changing that feature and the conditions that should remain fixed during a sample trial.
Vacuum drying removes solvent film effectively, but a pool trapped in a blind hole, closed corner or contact pocket has more liquid to remove. Part orientation and basket supports can create that pocket before drying begins.
No. A larger opening helps only when the existing mesh blocks the true outlet and the new opening still retains the smallest part. It cannot empty an upward-facing cavity or remove a support positioned beneath the low point.
The original liquid pocket should disappear under the unchanged machine cycle. The basket must still retain every part, preserve the intended contact surfaces and avoid creating a new wet location.
Yes. AUKE accepts trial quantities and repeat orders. A trial should use the intended parts, load and machine cycle so the result reflects the actual drainage and handling conditions.
Send one photograph of the wet area before unloading and one photograph of the complete loaded basket. Add the part or basket drawing, loaded weight and machine support dimensions when available.
We will map the wet location against the part orientation and basket supports. The discussion will identify the most plausible source, the basket feature worth changing, the tradeoff that change creates and the conditions to hold constant during the trial. If the pattern points away from the basket, we will say so.
Discuss the wet-part pattern with AUKEEmail: linda@auke-bott.com | Tel/WhatsApp: +86 182-6169-0816


